Acceptance Quality Limit (AQL) is used in acceptance-sampling schemes to select a sample and define acceptance and rejection criteria for a lot. The chosen AQL is one input to a sampling plan; the applicable standard, lot size, inspection level, sampling scheme and agreed defect criteria determine how the plan is applied.
1. Agree the inspection rules before production is released
Before inspection, buyer and supplier should agree the applicable sampling standard and edition, inspection level, AQL values, defect categories, product specification and the definition of a lot. Typical categories are critical, major and minor defects, but definitions and acceptance criteria must be product- and contract-specific. Do not assume one universal AQL applies to every product or market.
2. Determine the lot size and sample size
Identify the inspection lot and its quantity, then use the relevant sampling table and selected inspection level to find the sample-size code and sample size. Select units randomly across cartons or locations so the sample is not hand-picked by the factory. The inspector should record the lot, carton selection, sample quantity and any deviations from the agreed plan.
3. Inspect each sampled unit against defined criteria
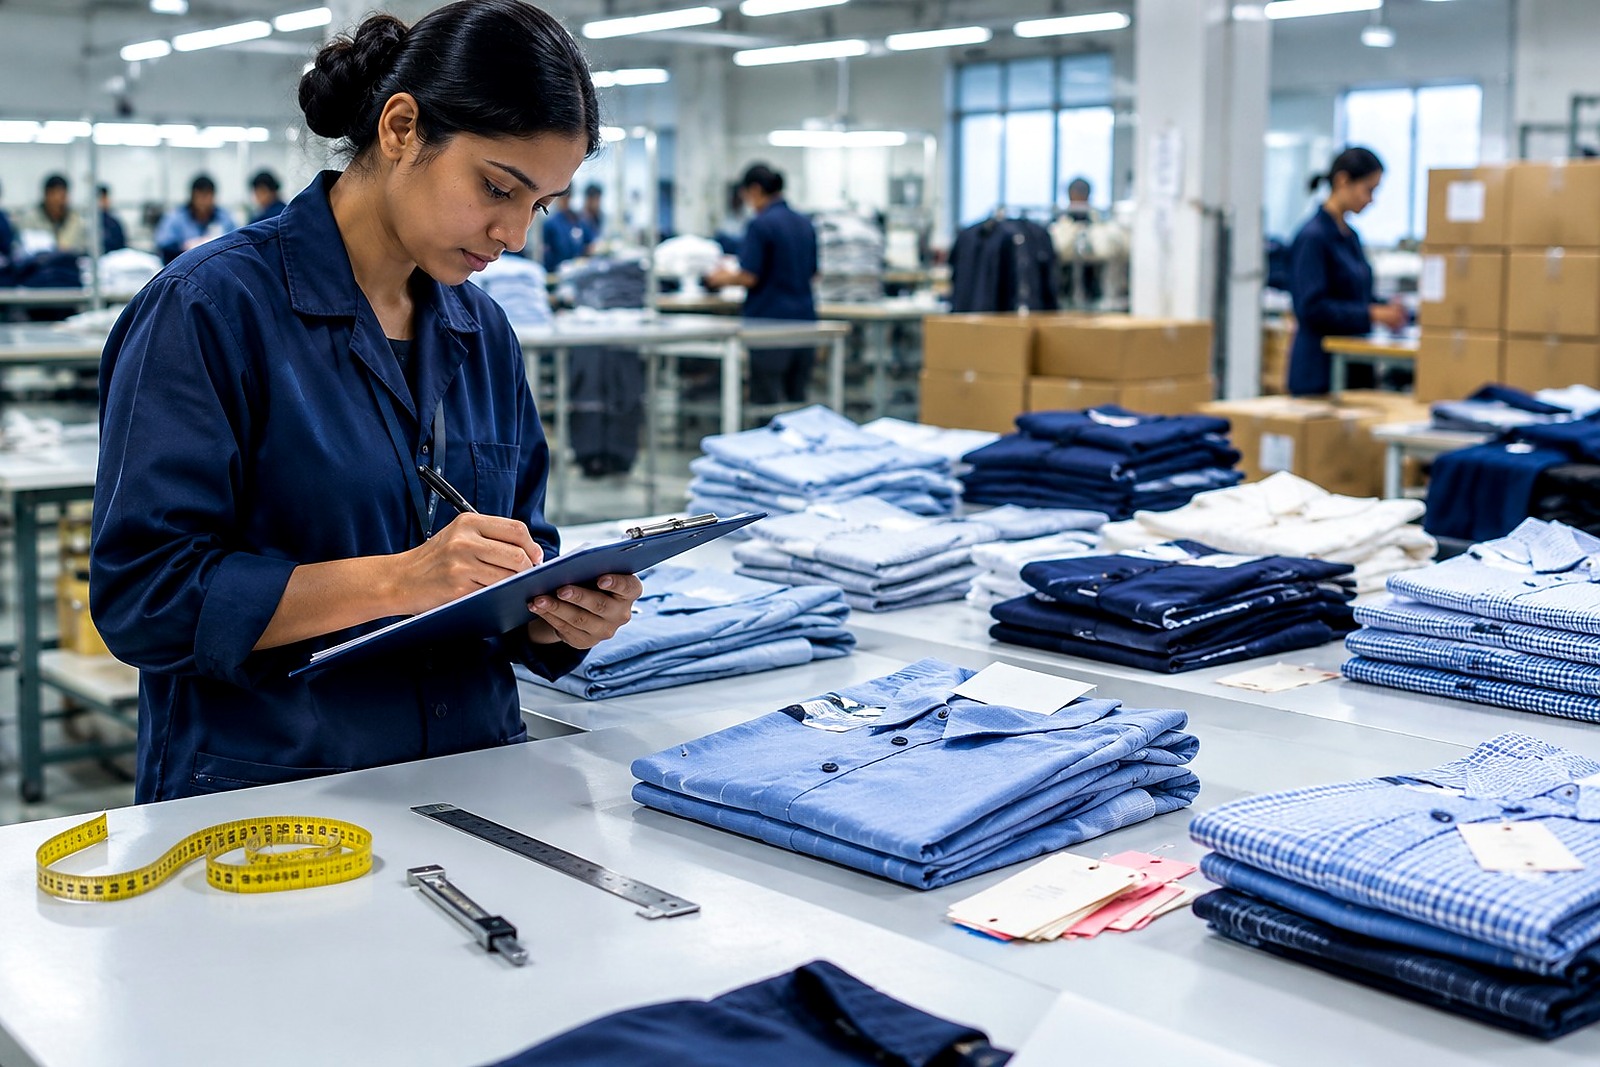
Check workmanship, dimensions, function, appearance, labeling, packaging and other specified requirements. Count nonconforming units and/or nonconformities in the way required by the selected plan. Keep objective evidence: defect descriptions, quantities, photographs, measurements and the requirement that each finding failed.
4. Compare results with the acceptance and rejection numbers
The sampling plan gives decision thresholds for the sample. If the observed result meets the plan's acceptance criteria, the lot may be accepted under that sampling plan; if it reaches the rejection criteria, the lot is not accepted under the plan. Follow the plan's exact decision rules—do not substitute a simple percentage calculation for the prescribed tables or confuse AQL with the actual defect rate in the sample.
If an inspection sample contains 80 units and 3 units are found nonconforming, the observed sample proportion is 3 ÷ 80 = 3.75%. That number alone does not determine pass or fail. The decision depends on the agreed sampling plan's sample size and acceptance/rejection numbers for the relevant defect category.
5. Report the decision and control the next action
A useful report records the sampling standard and edition, lot size, inspection level, AQL values, sample size, defect counts by category, acceptance/rejection criteria, photos, test results and final decision. If a lot is rejected, define containment, rework or sorting, corrective action and whether a re-inspection is required. Escalate repeat failures and consider whether normal, tightened or reduced inspection rules apply under the selected standard.
What AQL does—and does not—tell a buyer
- It does: provide a defined statistical sampling scheme for lot-by-lot decisions when used as specified.
- It does not: certify every unit, guarantee zero defects, replace safety testing, or make an unsuitable product specification adequate.
- It depends on: the standard and edition, lot definition, inspection level, selected plan, agreed defect classifications and correct random sampling.
Reference: ISO 2859-1:2026, Sampling procedures for inspection by attributes — Part 1: Sampling schemes indexed by acceptance quality limit (AQL) for lot-by-lot inspection. The current standard specifies single, double and multiple sampling plans; use the official standard and contract requirements to select the applicable plan.
Check the ISO 2859-1 standard page.
Need a sampling plan for your product and lot? Request an inspection and audit quote or contact info@qivglobal.com.